Piston vs Flow Meter vs Net-Weight Filling for Sauces: Which Dosing Principle Fits?

John senior engineer and founder
mia@gdhpmachine.com

A filler that looks suitable for a smooth, free-flowing sauce can become a poor fit when the production recipe is a hot, viscous tomato sauce with suspended pieces. The machine name may be the same, but the product path, valve, nozzle, feed system, and dosing principle are not interchangeable.

If those details are missed, the line can face blockage, particle damage, unstable cut-off, air pockets, and contaminated jar rims. A catalog accuracy figure cannot resolve a mismatch between the measuring method and the sauce’s actual flow behavior.

This guide compares piston, flow-meter, and net-weight filling by product viscosity, particulate geometry, declared fill basis, hot-fill conditions, container range, cleaning, and output. Use it to shortlist a principle, then confirm the final configuration with product-and-container trials.

Quick Answer

If the sauce is highly viscous, does not flow freely, or contains sizeable soft particulates, start with a piston filler because positive displacement can move a defined volume through a correctly sized product path.

If the sauce is homogeneous, pumpable, and suited to the selected meter technology, consider a flow-meter filler because the target dose can be set electronically without changing a metering cylinder.

If the commercial target is net mass, density varies, or each large fill represents substantial product value, consider net-weight filling because the load cell controls the mass delivered to the container rather than inferring it from volume.

First, Separate the Dosing Principle from the Product Pump

Buyers often use “pump filler” and “flow-meter filler” as if they describe the same architecture. They do not. The pump moves product; the dosing system decides when the target quantity has been delivered. A line may use a lobe or other positive-displacement pump to feed a flow meter, while a piston filler uses the piston cylinder itself as the metering chamber.

A piston system measures displacement volume. A flow-meter system measures flow through a sensor; depending on the technology, that may be volumetric flow or mass flow. A net-weight system measures the change in container weight on a load cell. Ask the supplier to identify both the feed method and the measurement method.

Engineering Note from a Sauce-Line Specification

One Europe food-sauce line specification called for stepper-driven rotary-pump dosing and stored filling recipes for repeat formats. The useful lesson is not that a rotary pump is universally preferable; it is that “pump filling” is a separate option and should not be mislabeled as flow-meter control unless a meter actually determines the dose.

Various food sauces

Five Decision Points for Choosing a Sauce Filling Principle

1. Sauce Flow Behavior and Particulate Geometry

If the sauce is non-free-flowing or carries pieces that need a wide, unobstructed passage, choose a suitably configured piston filler because the piston can draw and discharge a controlled volume under positive pressure.

“Contains particulates” is not a complete specification. Record the largest particle dimensions, particle concentration, shape, softness, and whether solids settle or float. The minimum internal diameter of the valve, manifold, hose, and nozzle must be assessed as one product path. Particle damage is also affected by valve geometry, pump shear, and fill speed—not merely by the dosing label.

If the sauce is smooth and continuously pumpable, a compatible flow meter can reduce the need for dose-specific cylinders. If irregular pieces can bridge the sensor tube or if the product separates during recirculation, a generic flow-meter recommendation is not enough; test the proposed meter bore and feed pump with the real recipe.

For broader product-state screening before comparing dosing systems, use the filling machine guide based on product and fill volume.

2. Declared Quantity, Density, and Temperature

If the label and process controls are based on volume, choose piston or compatible volumetric flow-meter dosing because both directly control a volumetric target. If the target is net mass, choose Coriolis mass-flow or net-weight control because either can measure mass without relying on a fixed density conversion.

Density can change between formulations and with temperature. That matters when a volumetric fill is converted into a weight claim. A piston stroke may remain mechanically consistent while the mass inside that volume changes. Conversely, a net-weight system is not automatically immune to unstable flow: poor cut-off, vibration, product stringing, or sauce settling on the jar rim can still affect the final result.

Do not compare “accuracy” percentages until each supplier states the measurement basis, target dose, product temperature, number of test cycles, calculation method, and whether the data came from the production sauce or a water test.

Put accuracy claims beside a legal-content benchmark

For prepacked products assessed under OIML R 87 (the same tolerable-deficiency schedule is used by the EU Directive 76/211/EEC), Table 2 sets the tolerable deficiency by declared quantity: 100–200 g/mL = 4.5% of Qn; 200–300 g/mL = 9 g/mL; 300–500 g/mL = 3%; 500–1,000 g/mL = 15 g/mL; and 1,000–10,000 g/mL = 1.5%. The inspection-lot average must be at least the declared quantity, and an individual pack must not exceed twice its applicable tolerable deficiency. These are legal metrology limits—not a filler’s repeatability specification.

That makes the comparison concrete. A 240 mL jar is in the 200–300 mL band, where the tolerable deficiency is 9 mL and the twice-T individual limit is 18 mL. Separately, a machine claim of ±0.5% at 240 mL equals ±1.2 mL, while ±1% equals ±2.4 mL. Ask the supplier to show mean, spread, and worst observed error from the same sauce, jar, temperature, and test method; never substitute a legal limit for a Factory Acceptance Test criterion.

For a flow-meter reference point, the Endress+Hauser Promass F 300 technical information lists liquid mass/volume-flow base accuracy of ±0.10% of reading, or ±0.05% with its PremiumCal option. That is a sensor-level figure measured on ISO 17025-traceable calibration rigs—not a complete sauce-filler result. Pump pulsation, entrained air, temperature, valve cut-off, and installation can produce a larger final dose error.

3. Hot-Fill Thermal Control

If viscosity rises quickly as the product cools, select the dosing principle only after specifying the complete heated path because a suitable meter or piston cannot compensate for cold spots in the hopper, pipework, valve, or nozzle.

Hot filling changes more than seal material. Temperature influences viscosity, density, stringing, pump load, and valve response. The design review should cover heating or recirculation, hopper agitation, insulation, stop-and-restart behavior, container heat resistance, closure timing, and controlled cooling. The hot filling machine buying guide explains how these choices connect across the complete line.

Food-safety classification adds another hard boundary. The U.S. 21 CFR Part 114 definition uses an equilibrium pH of 4.6 or below for an acidified food, while 21 CFR Part 113 covers low-acid canned foods above pH 4.6 when water activity is above 0.85. Those thresholds determine the process-control category; they do not prescribe one universal fill temperature. A process authority still has to set the scheduled thermal process for the recipe, container, closure, and heat-up/cool-down profile.

Hot filling machine filling sauce into glass jars

4. Container, Fill Range, and Tare Variation

If one line must cover many fill volumes, favor electronically adjustable flow-meter or net-weight targets when the product permits because the dose can be changed in the control recipe; however, bottle guides, nozzles, and fill height may still need adjustment. If the range is narrow and the sauce is difficult to move, a correctly sized piston cylinder may be the simpler choice.

For glass jars, ask how the proposed net-weight machine handles tare. Some systems weigh each empty container before filling; others rely on a configured tare or a separate weighing sequence. If empty-jar weight varies and the system controls gross weight only, that variation can carry into the calculated net content.

5. Output, Changeover, and Sanitation

If the line runs a stable, smooth recipe at sustained output, a compatible flow-meter architecture can be attractive because electronic dose settings support repeatable recipes. If recipes change between smooth and chunky sauces, choose the principle and product path around the hardest product because the easiest product rarely determines the real limitation.

Output must be calculated at the actual fill volume and product temperature. Thick sauce intake time, fine-fill or cut-off time, load-cell settling time, nozzle count, container indexing, and upstream supply pressure all affect cycle time. For the relationship between dosing architecture and automation level, see these fully automatic filling machine options.

Use comparable speed and giveaway numbers

The published GDHP automatic-filler guide places medium/high-speed versatile lines at 2,000–8,000 bottles per hour and continuous rotary lines at up to 24,000+ bottles per hour; sauces and condiments are listed in the medium/high-viscosity application group. These are category ranges, not a promise for a particular sauce. A separate published GDHP project page reports a cleaning-paste line designed around ±1% accuracy and 2,800 bottles per hour at 240 mL; that nameplate equals 672 L/h before stops, changeovers, and cooling constraints. Treat it as a project-specific reference and request the same basis for your product.

For a transparent cost check, calculate giveaway in product units before comparing machine prices. If 100,000 jars are filled to an average 1% overfill at 240 mL, the arithmetic giveaway is 240 L; at 0.5% it is 120 L. This is an illustrative planning calculation, not a measured result. Multiply the volume by your sauce cost and add labor, utilities, cleaning, rejects, and downtime to compare total cost of ownership.

Sanitary review should identify drainability, dead legs, seal access, valve disassembly, cleaning chemistry, rinse verification, and allergen-change procedures. “CIP-capable” is not the same as a validated CIP process. Piston seals and valves need inspection access; meter systems still need a cleanable pump, piping, and cut-off valve; load-cell platforms need protection from product accumulation and washdown effects.


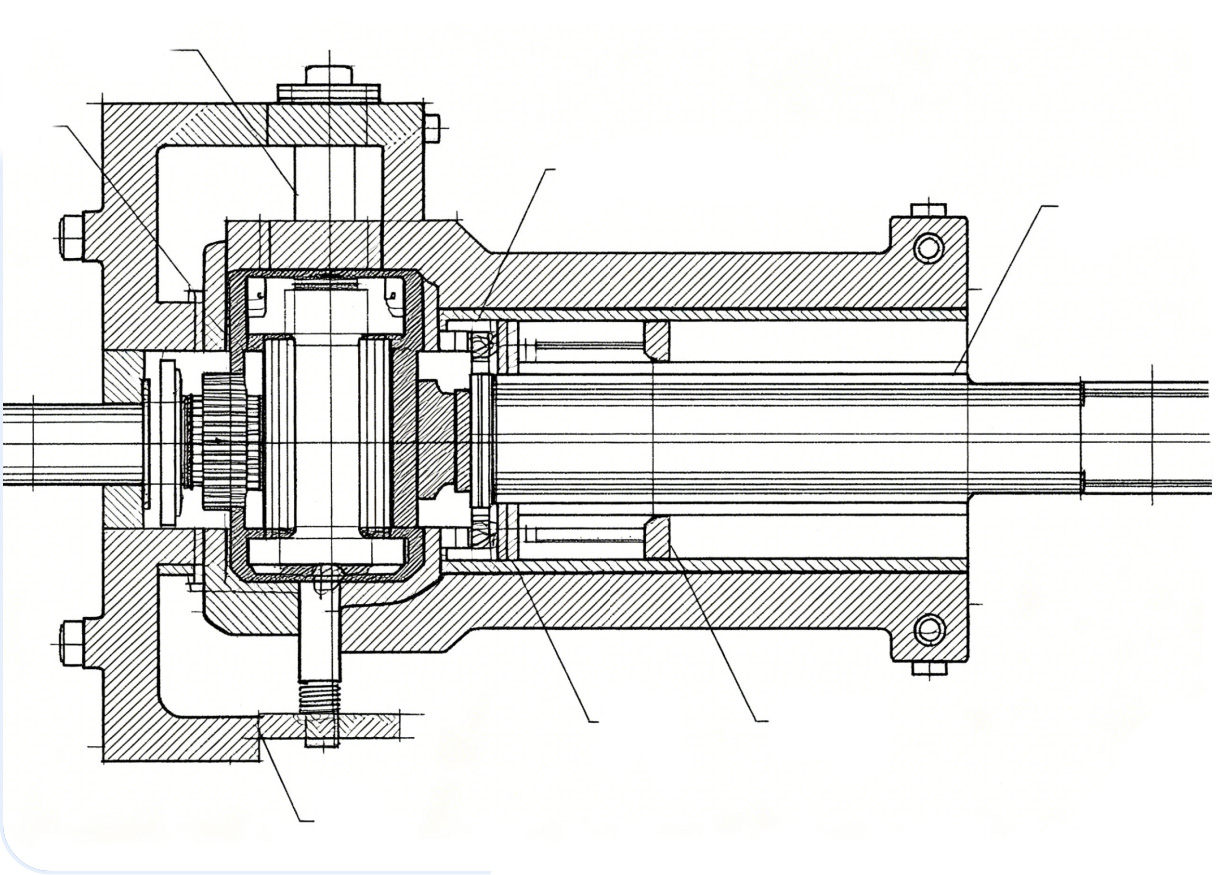
Piston Pump

Where Each Principle Fits—and Where It Does Not

Choose a Piston Filler for Viscous or Particulate Sauces

Piston filling is usually the first principle to test for thick tomato sauce, salsa, pesto, jam, and similar products that need positive displacement. The cylinder draws a set volume from the hopper and discharges it through the product valve and nozzle. Read how volumetric filling machines work for a deeper explanation of the dosing cycle.

The important qualification is “correctly configured.” The valve port, hose, manifold, and nozzle must suit the largest particle and desired particle integrity. Hopper agitation should keep solids distributed without over-shearing the sauce. Anti-drip or shut-off design must be tested at both the start and end of a production run, when temperature and head pressure may differ.

A piston filler may be the wrong choice when the required dose range is too broad for one cylinder, frequent manual teardown is unacceptable, or the commercial target must be controlled directly by mass. Seal wear and trapped air should also be part of the maintenance and accuracy plan.

Choose a Flow-Meter Filler for Smooth, Pumpable Sauces

A flow-meter filler can suit smooth tomato sauce, syrups, dressings, and other homogeneous products that can be delivered in a stable stream. Because the target is set in the control system, recipe changes do not require changing a piston cylinder. The product pump, meter, valve, and nozzle still have to be sized as one hydraulic system.

Do not approve a quote that says only “flow meter.” An electromagnetic meter normally requires an electrically conductive product. A Coriolis meter measures mass directly but has its own tube geometry, pressure-drop, cleanability, and cost considerations. Other meter types have different limits. The supplier should name the sensor principle and document why it fits the recipe.

A flow-meter filler is not the default for chunky sauce. Small suspended solids may be acceptable in a correctly sized system, but particle shape, concentration, settling, and the pump’s shear profile must be tested. When product viscosity or conductivity moves outside the proposed meter’s validated range, dosing stability can suffer.

Choose Net-Weight Filling When Mass Is the Controlling Requirement

In net-weight filling, the container is supported on a load cell while the product is dispensed. The control system stops the bulk fill and fine-fill stages as the measured mass approaches the target. This can be useful for premium sauces, bulk foodservice packs, or recipes whose density varies enough to make volume-to-weight conversion inconvenient.

The trade-off is that the weighing environment becomes part of the filling system. Conveyor vibration, container contact with guides, air movement, sauce strings, and a slow-closing valve can affect the reading. For a true net result, the tare strategy must match actual container-weight variation.

Net-weight control does not mean zero giveaway, nor is it automatically the fastest or most accurate option for every sauce. Compare the final distribution from a controlled production trial, not the sensor resolution printed in a component datasheet.

Piston vs Flow Meter vs Net-Weight: Comparison Matrix

Decision factorPiston fillerFlow-meter fillerNet-weight filler
What is measured?Displaced chamber volumeVolumetric or mass flow, depending on meter typeChange in container mass on a load cell
Recommended scenarioViscous or non-free-flowing sauces; particulate products when passages and valves are correctly sizedHomogeneous, pumpable sauces compatible with the chosen sensor and pumpMass-declared products, large fills, variable density, or high-value formulations
Not recommended without further testingProducts whose pieces exceed or bridge the product path; highly aerated sauce; very broad dose range on one cylinderLarge or irregular particulates; separation-prone recipes; unknown conductivity for an electromagnetic meterUnstable or flexible containers; high-vibration installations; lines where weighing and settling time cannot meet the cycle
Temperature and densityControls volume; mass per dose can move with densityDepends on whether the meter measures volume or massControls delivered mass; flow and cut-off still require thermal stability
ChangeoverStroke can be adjusted; a large range may require another cylinder or hardwareTarget is electronic; product and container hardware may still changeTarget is electronic; tare routine and container support must be verified
Main validation riskIncomplete intake, seal wear, entrained air, valve timing, particle damageWrong meter type, insufficient straight-run or feed conditions, sensor fouling, pressure dropVibration, tare error, product cut-off lag, sauce on the container, load-cell settling
Cleaning focusCylinder, piston seals, rotary/check valves, manifold, nozzlesMeter tube, feed pump, piping, valves, nozzlesProduct path plus load-cell platform and spill protection

Three Common Wrong Choices

  1. Choosing by viscosity alone. Two sauces with similar apparent viscosity can behave differently because one contains particles, entrained air, fibers, or a yield stress. Give the supplier samples and a product specification, not only a cP value.
  2. Assuming every flow meter is equivalent. A quote that omits the sensor type, bore, materials, operating range, and feed-pump conditions leaves the most important compatibility questions unanswered.
  3. Using a water test to accept a sauce filler. Water does not reproduce sauce intake, particle passage, thermal loss, stringing, aeration, or cleaning behavior. It can check basic machine motion, but it cannot prove product performance.

FAT Checklist: Validate the Decision Before Shipment

Define acceptance criteria before the Factory Acceptance Test. Avoid a vague requirement such as “high accuracy”; agree on the test conditions and the calculation method.

  • Product: use the actual recipe or an agreed substitute with documented viscosity, density, particulate dimensions, concentration, and temperature behavior.
  • Containers: test the smallest and largest formats, including normal tare variation, neck finish, and heat resistance.
  • Operating window: run at minimum and maximum fill volumes, normal speed, intended hot-fill temperature, and realistic hopper level.
  • Start-stop behavior: inspect the first fills after warm-up, a planned pause, and restart; check temperature loss, settling, dripping, and nozzle blockage.
  • Dose evaluation: agree on sample size, reference instrument, units, mean error, spread, acceptable short fills, and allowable overfill.
  • Product quality: inspect particle integrity, phase separation, aeration, foaming, jar-rim cleanliness, and closure area.
  • Cleaning and changeover: demonstrate draining, disassembly or CIP sequence, inspection points, recipe recall, and format adjustment.
  • Line integration: confirm hopper supply, no-bottle/no-fill logic, capping timing, rejection method, cooling, alarms, and upstream/downstream interlocks.
Pre-shipment inspection

Choose with a Product Trial, Not a Label

To compare piston, flow-meter, and net-weight filling for your sauce, prepare the operating parameters listed above and request a documented trial plan. GDHP can review the product, container, output, hot-fill process, sanitation method, and factory layout before recommending an option from its filling machine range.

Ask for a recommendation that states not only which principle fits, but also why the other two are less suitable under your stated conditions.

Have questions? Reach out to us, and we will provide you with a perfect solution.

FAQ

A piston filler is usually the first option to trial because it can provide positive displacement through a wide product path. The final valve and nozzle sizes must be checked against the largest particle, particle concentration, and required product integrity.

It can when the tomato sauce is homogeneous and pumpable and the selected meter is compatible with its conductivity, viscosity, temperature, and solids. “Hot fill” alone does not prove compatibility; the complete heated feed and cut-off system must be tested.

No. It directly controls mass, which may be the relevant commercial target, but final performance still depends on tare handling, vibration, load-cell settling, product flow, and valve cut-off. Compare trial data under the same sauce, container, dose, speed, and temperature conditions.

The cylinder still displaces a defined volume, but large viscosity changes can affect cylinder intake, air entrapment, valve timing, and cut-off. If the chamber does not fill completely or the sauce strings from the nozzle, the delivered result can change.

Not normally without substantial changes. Some modular platforms can accept different pumps, meters, or weighing controls, but the frame, valves, nozzles, software, and container handling must be designed for that scope. A machine optimized for the most difficult recipe is usually more realistic than a claim of universal compatibility.

Provide the sauce recipe category, viscosity at filling temperature, density, largest particle dimensions and concentration, fill temperature, minimum and maximum dose, container drawings and samples, closure, target output, declared quantity basis, cleaning method, and available utilities. Also state which characteristics must remain intact after filling.

Build Your Custom Solution

Your information is secure - we respect your privacy and will only use these details to contact you.

Build Your Custom Solution